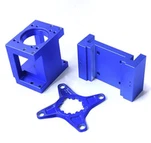
Impact of Aluminum Alloy Grade and Structural Complexity on Housing Deformation
1. Influence of Aluminum Alloy Grade
Different aluminum alloys exhibit distinct mechanical, thermal, and metallurgical properties that directly affect machining stability and deformation susceptibility.
表格
| Alloy Series | Typical Grades | Key Properties Affecting Deformation | Deformation Risk |
|---|---|---|---|
| 1xxx (Pure Al) | 1050, 1100, 1060 | High ductility, low strength, excellent thermal conductivity | High-soft material deflects easily under cutting forces; poor dimensional stability |
| 2xxx (Al-Cu) | 2024, 2014, 2017 | High strength, significant residual stresses from heat treatment | Very High-2024-T351 particularly prone to warping due to quenching stresses |
| 3xxx (Al-Mn) | 3003, 3004 | Moderate strength, good formability, low residual stress | Low-stable during machining; minimal distortion tendency |
| 5xxx (Al-Mg) | 5052, 5083, 5754 | Good corrosion resistance, work-hardening tendency | Moderate-strain hardening during machining can induce spring-back |
| 6xxx (Al-Mg-Si) | 6061, 6063, 6082 | Excellent machinability, heat-treatable, balanced properties | Moderate-T6 temper has residual stresses; T651 stress-relieved is preferred |
| 7xxx (Al-Zn-Mg) | 7075, 7050, 7005 | Highest strength among wrought alloys, high residual stresses | Very High-7075-T6 exhibits severe distortion; requires stress relief before finish machining |
| Cast Alloys | A380, ADC12, A356 | Inhomogeneous microstructure, porosity, silicon phases | Moderate to High-porosity causes localized weak points; uneven machining response |
Critical Observations:
Residual Stress Level: Heat-treated alloys (2xxx, 6xxx-T6, 7xxx) retain quenching stresses that release asymmetrically during material removal, causing unpredictable warping.
Thermal Expansion Coefficient: All aluminum alloys share similar high thermal expansion (~23×10⁻⁶/°C), but alloys with higher strength require more aggressive machining parameters, generating more heat and thermal gradients.
Elastic Modulus: Lower modulus (69 GPa vs. steel's 210 GPa) means aluminum deflects more under identical cutting forces, amplifying any structural weakness.
2. Influence of Structural Complexity
Geometric complexity determines how machining forces, thermal effects, and stress redistribution manifest as visible deformation.
表格
| Complexity Factor | Deformation Mechanism | Risk Level |
|---|---|---|
| Thin Walls (<2 mm) | Low rigidity causes elastic deflection under cutting forces; thermal gradients create buckling | Very High |
| Deep Cavities/High Aspect Ratio | Long tool overhangs increase vibration; uneven material removal creates unbalanced stresses | High |
| Asymmetric Geometry | Non-uniform mass distribution leads to differential cooling and stress release | High |
| Internal Ribs & Bosses | Stress concentration at junctions; differential shrinkage between thick and thin sections | Moderate to High |
| Large Flat Surfaces | "Potato chip" effect from residual stress release; thermal bowing | Moderate |
| Cross-Holes/Intersecting Features | Interruption of material continuity creates weak points for distortion | Moderate |
| Tight Tolerances on Multiple Datums | Cumulative error from multiple setups; datum shift between operations | High |
| Integrally Machined Enclosures | Monolithic removal of material from solid block maximizes stress redistribution | Very High |
3. Synergistic Effects: Alloy × Complexity
The combination of material grade and geometry creates specific deformation scenarios:
表格
| Scenario | Example | Deformation Characteristic |
|---|---|---|
| High-strength alloy + thin walls | 7075-T6 aerospace housing with 1.5 mm walls | Severe warping; requires stress relief + vacuum fixturing + cryogenic machining |
| Cast alloy + complex internal geometry | A380 electronic enclosure with deep ribs | Porosity-induced localized distortion; unpredictable dimensional variation |
| Soft alloy + large flat surface | 1100 aluminum faceplate | Thermal bowing and clamping imprint; difficult to maintain flatness |
| Heat-treated alloy + asymmetric removal | 6061-T6 bracket with one-sided pocket | Twist deformation upon unclamping; requires symmetric machining sequence |
| Work-hardening alloy + deep cavity | 5083 marine housing | Gradual hardness increase during machining causes variable cutting response |
4. Mitigation Strategies by Material-Complexity Combination
表格
| Alloy Category | Structural Complexity | Recommended Approach |
|---|---|---|
| High residual stress (2xxx, 7xxx, 6xxx-T6) | Any complexity | Mandatory stress-relief temper (T651, T7351); rough machine → heat treat → finish machine |
| Cast alloys | Complex internal features | NDT inspection for porosity; adaptive machining with force feedback; increased stock allowance |
| Soft alloys (1xxx, 3xxx) | Thin walls | Vacuum fixturing; minimum cutting forces; temporary reinforcement with dissolvable supports |
| Work-hardening (5xxx) | Deep features | Frequent tool changes; optimized speeds to minimize strain hardening; climb milling preferred |
| All alloys | Large thin-walled housings | Symmetrical material removal; temporary ribs left until final pass; thermal stabilization periods |
5. Design-for-Manufacturing Guidelines
To minimize deformation in custom aluminum housings:
Material Selection:
For general precision: 6061-T651 (stress-relieved) offers optimal balance
For high strength with stability: 7050-T7451 (aerospace grade, controlled quenching)
For cast complex shapes: A356-T6 (fine grain, reduced porosity) over A380
Geometry Optimization:
Maintain wall thickness ≥3 mm where possible; transition gradually between thick and thin sections
Add temporary process ribs for machining stability; remove in final operation
Design symmetric features to balance material removal
Specify tolerances relative to a single primary datum to minimize setup changes
Process Specification:
Define machining sequence: rough → semi-finish → stress relief (if needed) → finish
Specify fixture type (vacuum, conformable, hydraulic) based on wall thickness
Require thermal stabilization before critical measurements
Summary
表格
| Factor | Impact on Deformation | Controllability |
|---|---|---|
| Alloy grade | Determines residual stress, strength, thermal response | High-proper temper selection essential |
| Structural complexity | Determines rigidity, thermal mass distribution, stress release pattern | Moderate-DFM can optimize geometry |
| Machining sequence | Affects stress redistribution symmetry | High-process engineering critical |
| Fixturing method | Determines clamping-induced distortion | High-technology selection important |
| Thermal management | Controls expansion gradients | Moderate-environmental control required |
Conclusion: Both aluminum alloy grade and structural complexity significantly influence housing deformation in custom machining. The interaction is multiplicative rather than additive: a high-strength alloy with complex thin-walled geometry presents exponentially greater challenges than either factor alone. Successful production requires material-specific process design-selecting appropriate tempers, implementing stress-relief protocols, and tailoring machining strategies to geometric constraints. Finite element simulation of machining distortion, validated by prototype trials,